Product successfully added to your shopping cart
Quantity
Total
There are 0 items in your cart. There is 1 item in your cart.
Total products
Total shipping To be determined
Total
BMC A Series
Manufacturers
BMC A Series
 View larger
Warning: Last items in stock!
New product
ARP 8740 steel crankshaft main studs for BMC A-Series engines.
ARP lists this kit for the BMC A-Series ("BMC A-series"), with no engine code, model or year given. Part number 206-5401 is specific to this application.
As built, these main caps rest on the manufacturer's original hardware, which the kit's 7/16 inch studs replace.
In a bottom end, the main bearings absorb the thrust of the connecting rods at every combustion, and it is the main caps, clamped to the block, that hold the crankshaft in place. When their clamping gives way, the cap works on its parting line: the mating faces become marked, then the bearing bore distorts.
Kit 206-5401 contains ARP 8740 steel studs, 7/16 inch, which go into the block by hand only, after the threads have been cleaned. The caps, washers and nuts follow, coated with ARP Ultra-Torque rather than engine oil, then tightening in three equal passes, in the order set by the engine manufacturer, up to 108 Nm (80 ft-lb). Material: 8740, a chrome-moly steel that ARP specifies at 200,000 psi tensile strength, with threads rolled after heat treatment. Factory-fitted fasteners usually belong to classes 10.9 and 12.9, with 150,800 to 176,900 psi minimum tensile strength. The kit strengthens the main cap fixing of built BMC A-Series engines; no strength figure is published for this part number.
| Part number | Brand | Grade / material | Nut | Thread |
| ARP-206-5401 | ARP | 8740 steel | Nut | 7/16 inch |
| Reference | Pass 1 | Pass 2 | Pass 3 |
| ARP-206-5401 | 36 Nm | 72 Nm | 108 Nm |
The studs are fitted into the block by hand, with no torque tightening. The ARP instruction sheet accepts a thread locker when the installation is to be permanent, provided the nuts are fully tightened before it hardens.
The nuts are tightened following the order set by the manufacturer for the caps; every step is given in the ARP instruction sheet.
After moving to stronger fasteners, the size and roundness of the main bearing bores are checked; if needed, the main bearing line is honed with the final fasteners and lubricant fitted.
Torque figures taken from the ARP 206-5401 instruction sheet, in the revision in force on the day of publication. In the event of any difference, the manufacturer's instruction sheet prevails. Read the ARP 206-5401 instruction sheet
Tightening is done with ARP assembly grease: the torque figures in the table were established with it, not with engine oil.
| Buy the ARP assembly grease → |
 | ARP, short for Automotive Racing Products, was born in the early 1970s on the initiative of Gary Holzapfel, an engineer from the aerospace sector, in response to the engine failures caused in racing by inadequate fasteners. Today the brand produces thousands of part numbers in California, offered in several materials depending on the application. |
| Criterion | Original fasteners | Reinforced ARP studs |
 | 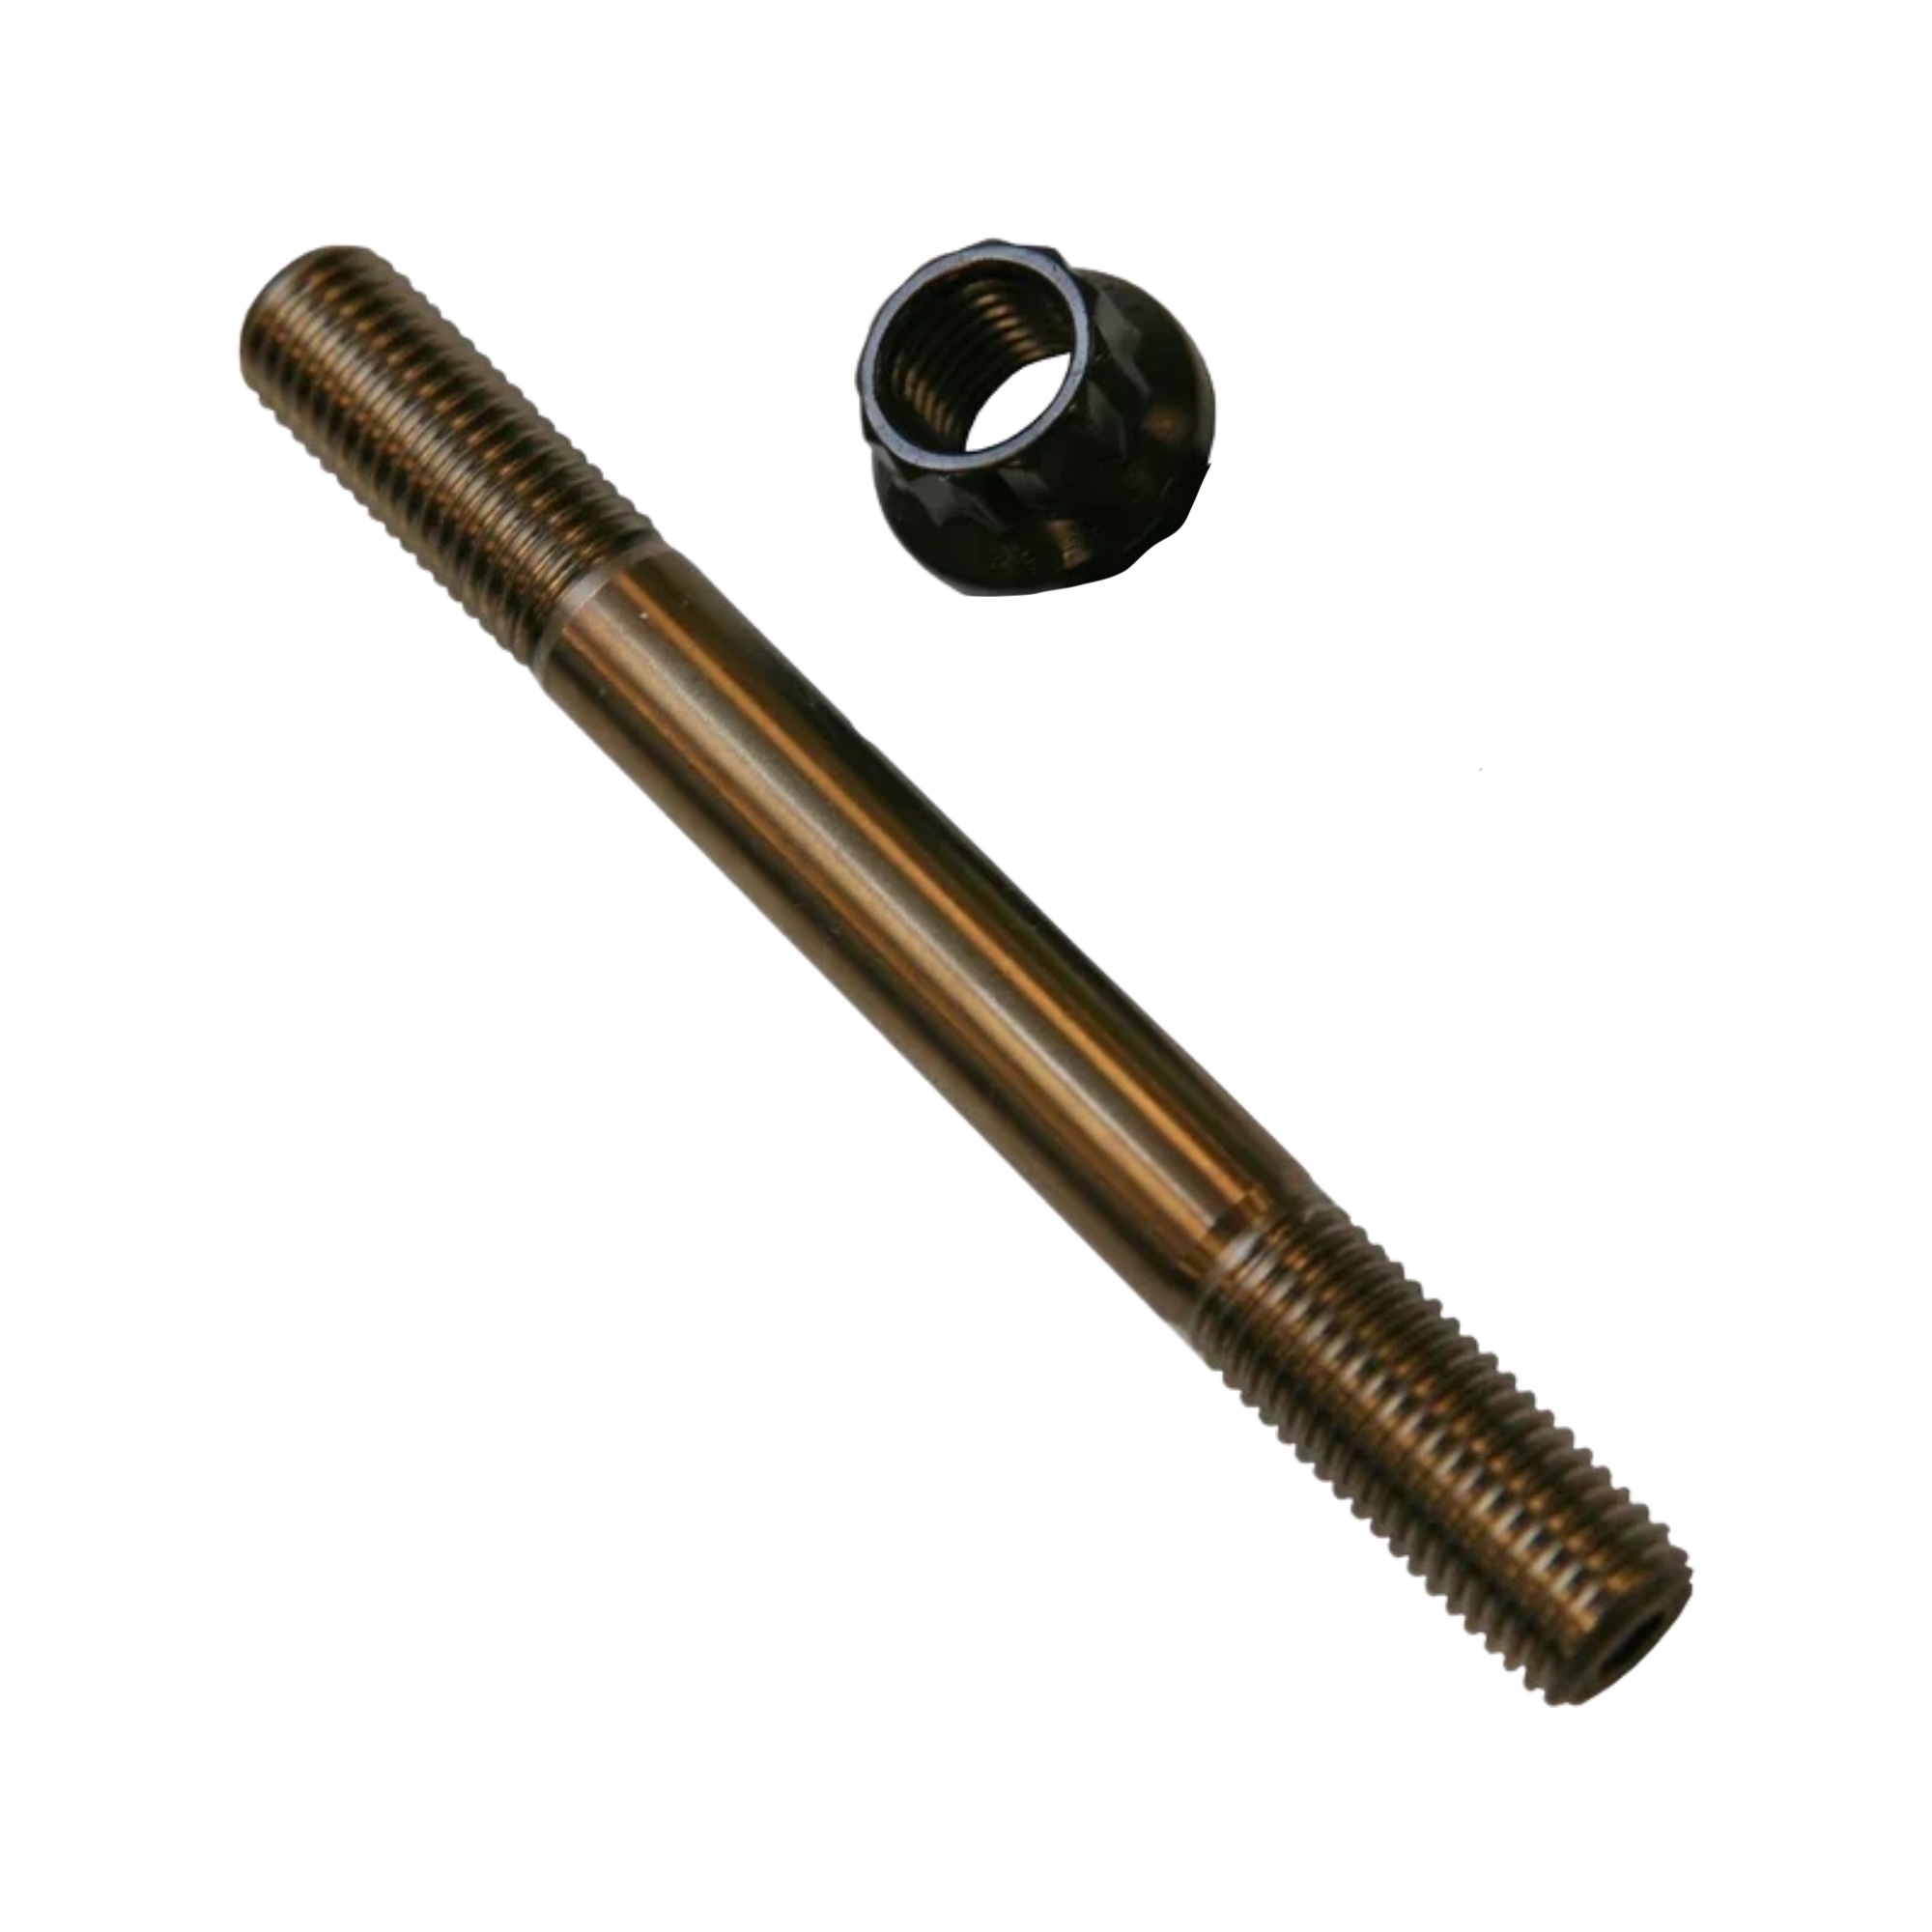 | |
| Cap fixing | Varies with the engine | Stud fixed in the block, nut tightened on the cap side |
| Steel | Varies with the engine | 8740 chrome-moly steel, heat-treated for strength |
| Seating the cap | Varies with the engine | Cap located by the studs already screwed in |
| Model | Engine code | Power | Years |
| BMC, A-Series engines (application declared by ARP) | A-Series |
The bearings of a built A-Series engine work harder. A few ARP studs cost little next to replacing a crankshaft or a block.